Blog
Signature Lawn and Landscape LLC
China Top 10 Syrup Clarification Equipment Manufacturers?
China’s syrup clarification equipment sector serves sugar refineries, beverage plants, pharmaceutical facilities, and starch-syrup producers. This article examines ten notable Chinese manufacturers through practical purchasing criteria. These include clarification efficiency, filtration accuracy, throughput, automation, hygienic design, after-sales support, and documented operating experience.
Market reports from Grand View Research and Mordor Intelligence indicate steady growth in food-processing equipment and liquid filtration demand. However, they rarely isolate syrup clarification as a separate category. That limitation matters. Buyers should avoid treating broad filtration statistics as direct proof of syrup-equipment sales. A supplier’s real capability appears in clearer details: reduced turbidity, stable flow, lower filter-cloth consumption, and clean syrup leaving the vessel.
James C. P. Chen, author of the Cane Sugar Handbook, emphasized that “clarification is one of the most important operations in sugar manufacture.” His observation remains relevant. Poor clarification can darken syrup, shorten membrane life, and increase cleaning frequency. Good equipment behaves quietly. It controls temperature, residence time, pressure, and solids removal without damaging product quality.
The following manufacturers are assessed with a balanced approach. Public certifications, project records, technical documents, and customer support are considered together. Some company information is incomplete or difficult to compare. Therefore, this ranking is not absolute. It is a practical starting point for engineers and procurement teams seeking reliable syrup clarification solutions in China.
Definition and Role of Syrup Clarification Equipment
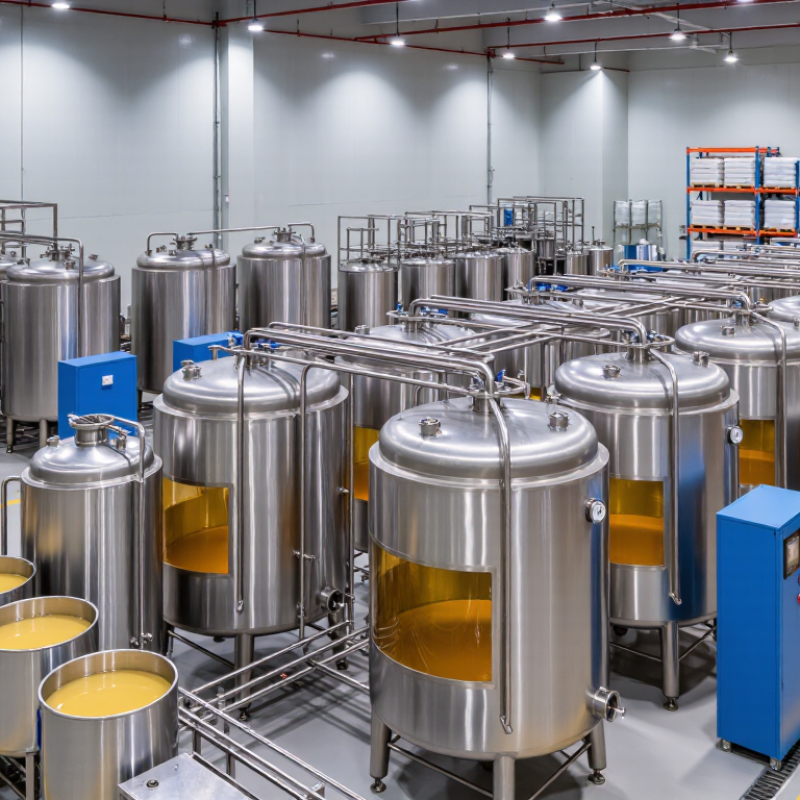
Syrup clarification equipment removes suspended particles, insoluble residues, and some haze-forming materials before filling or further processing. Its role is practical: protect product appearance, reduce contamination risks, and support consistent dosing. Typical systems use filter housings, depth filters, cartridge filters, or centrifugation. Selection depends on viscosity, temperature, sugar concentration, and required flow rate.
The WHO Guidelines for Drinking-water Quality emphasize that clear water is not automatically microbiologically safe. This lesson also applies to syrup production. A bright syrup may still contain microorganisms or dissolved impurities. The WHO Good Manufacturing Practices guidance treats water quality and process control as critical manufacturing concerns. FDA process-validation guidance also recommends lifecycle control, including process design, qualification, and continued verification. Operators should therefore check turbidity, pressure loss, microbial results, and filter integrity. Visual inspection alone is weak evidence.
Tips: Match the filter rating with the syrup’s viscosity. Record inlet and outlet pressure during every batch. Replace filters according to validated limits, not habit. The UNICEF and WHO Joint Monitoring Programme reported that 2.2 billion people lacked safely managed drinking water in 2022. That figure highlights why water quality deserves strict attention. In my experience, over-filtration can waste syrup and slow production. Under-filtration creates greater trouble. A perfect setup is rarely permanent; raw materials, temperature, and operator practice can change its performance.
China Top 10 Syrup Clarification Equipment Manufacturers? - Definition and Role of Syrup Clarification Equipment
| Rank | Anonymous Manufacturer Profile | Primary Equipment Configuration | Clarification Principle | Typical Throughput | Typical Filtration Range | Typical Operating Temperature | Recommended Product Role | Common Construction Material |
|---|---|---|---|---|---|---|---|---|
| 1 | Profile A | Multi-bag filter housing | Depth or surface filtration removes suspended particles before filling or concentration. | 10–120 m³/h | 1–100 μm | Ambient–90°C | High-volume prefiltration | 304 or 316L stainless steel |
| 2 | Profile B | Cartridge filter system | Pleated or melt-blown cartridges retain fine particles and protect downstream equipment. | 2–50 m³/h | 0.2–25 μm | Ambient–80°C | Fine polishing filtration | 316L stainless steel with food-grade seals |
| 3 | Profile C | Plate-and-frame filter press | Pressure-driven filtration separates insoluble solids from viscous syrup. | 0.5–30 m³/h | 5–50 μm | 40–95°C | Clarification of turbid or solids-rich syrup | 304 stainless steel; 316L wetted parts |
| 4 | Profile D | Self-cleaning automatic filter | Automatic backwashing or scraping maintains flow with limited manual intervention. | 10–150 m³/h | 10–100 μm | Ambient–120°C | Continuous production lines | 316L stainless steel |
| 5 | Profile E | Rotary vacuum drum filter | Vacuum-assisted cake filtration continuously removes suspended solids from process liquor. | 5–80 m³/h | 10–150 μm | 40–90°C | Large-scale continuous clarification | 304 stainless steel with corrosion-resistant internals |
| 6 | Profile F | Diatomaceous earth filter | Filter-aid media forms a porous layer that captures fine haze and insoluble matter. | 1–25 m³/h | 0.5–10 μm | 30–80°C | High-clarity syrup polishing | 316L stainless steel |
| 7 | Profile G | Decanter centrifuge | Centrifugal force separates dense suspended solids from liquid syrup. | 2–60 m³/h | Approximately 5–50 μm solids | Ambient–95°C | Rapid solids removal with low filter consumption | 316L stainless steel wetted zone |
| 8 | Profile H | Disc-stack centrifuge | High centrifugal acceleration separates very fine suspended particles from low-viscosity syrup. | 1–30 m³/h | Approximately 0.5–10 μm solids | Ambient–90°C | Fine clarification and continuous separation | 316L stainless steel |
| 9 | Profile I | Ultrafiltration system | A semi-permeable membrane retains colloids, macromolecules, and suspended impurities. | 0.5–20 m³/h | Typically 0.01–0.1 μm equivalent pore range | 20–60°C | Colloid reduction and high-grade clarification | 316L stainless steel and polymeric membranes |
| 10 | Profile J | Activated-carbon clarification vessel | Adsorption reduces color bodies, odors, and selected organic impurities before final filtration. | 1–40 m³/h | Follow-up filtration commonly 1–25 μm | 30–80°C | Color and odor improvement with polishing filtration | 316L stainless steel |
Key Technologies Used in Syrup Clarification
China Top 10 Syrup Clarification Equipment Manufacturers?
When comparing China’s top ten syrup clarification equipment manufacturers, buyers should examine process design, not catalog capacity. Syrup often enters clarification at 60–85°C, depending on concentration and product sensitivity. Controlled heating lowers viscosity and helps filters capture suspended particles. Excessive heat can darken syrup or damage flavor compounds. Pilot testing matters.
A typical line combines coarse screening, conditioning, and fine filtration. Centrifugal clarifiers remove heavier solids quickly. Plate-and-frame or pressure-leaf filters provide deeper polishing. Membrane systems can reduce fine colloids, but fouling remains real. Differential-pressure gauges, sanitary pumps, and automated backwashing improve process control. Food-contact steel, smooth welds, and validated clean-in-place cycles are essential. They protect hygiene and reduce downtime.
Reliable manufacturers should document particle retention, flow stability, energy use, and cleaning performance. Ask for test data using syrup with similar Brix, color, and viscosity. Laboratory turbidity alone can mislead. Operators also need clear alarms and easy access to filter elements. Real plants are less tidy. Sugar crystals, foam, and changing raw materials expose weak designs. I would question any promise of zero maintenance. Seals wear, membranes foul, and calibration drifts. Good equipment allows adjustment, records operating trends, and supports traceable replacement parts.
Evaluation Criteria for Selecting Chinese Manufacturers
Selecting among China’s top syrup clarification equipment manufacturers requires more than comparing prices. Mordor Intelligence’s 2024 Food Processing Equipment report estimates the global market will exceed USD 70 billion by 2029. That growth increases supplier choices, but not necessarily quality. Buyers should verify processing capacity, syrup viscosity, target turbidity, filtration accuracy, and cleaning requirements before requesting quotations. A factory test using real syrup is more reliable than a polished brochure.
Stainless steel contact surfaces should meet food-grade requirements, with documented material certificates and weld inspection records. Ask for flow-rate data, pressure limits, filter-life estimates, and CIP validation procedures. The equipment should maintain stable performance near the planned production rate, not only during short demonstrations. ISO 22000-based food-safety systems can support supplier evaluation, but certification alone proves little about equipment durability. Look for batch records, calibration controls, traceability, and clear spare-parts support.
Supplier experience matters. Review installations handling similar sugar concentration and temperature ranges. Request references, maintenance response times, and operator training details. Total cost should include energy use, consumables, downtime, and replacement filters. This is where many evaluations become weak. A cheaper unit may create higher losses through syrup retention or frequent cleaning. Independent inspection is worthwhile, although smaller projects may struggle to justify it. A practical scorecard should weigh technical performance, documentation, after-sales service, delivery control, and lifecycle cost rather than purchase price alone.
China’s Top 10 Syrup Clarification Equipment Manufacturers
China’s Top 10 Syrup Clarification Equipment Manufacturers are best assessed through performance, service, and process knowledge. A strong supplier should understand sugar concentration, syrup temperature, viscosity, and impurity load. These details affect filter selection and production stability. Plate filters suit many standard lines. Candle filters can support finer clarification. Membrane systems may help when lower thermal exposure is important.
Experienced manufacturers usually provide pilot testing before final equipment selection. This step matters. Syrup can look clear in a sample but behave differently at full scale. Engineers should check flow rate, pressure loss, cleaning cycles, gasket materials, and food-contact compliance. Stainless steel construction is expected, but surface finish still deserves attention. Poor welds can create cleaning problems.
The best ten should also offer useful commissioning support, spare parts, and operator training. Clear documents are a practical sign of reliability. However, no ranking is perfect. Marketing claims may not match a factory’s daily performance. Buyers should request recent references, test data, and a realistic maintenance schedule. Energy use deserves review too, especially for heated syrup systems. A cheaper filter may create higher labor costs later. That mistake is common. Manufacturers that listen carefully to the process often deliver better results than those selling one standard design.
Applications, Maintenance, and Industry Trends
China Top 10 Syrup Clarification Equipment Manufacturers: Applications, Maintenance, and Industry Trends
Syrup clarification equipment serves pharmaceutical, beverage, confectionery, and liquid food production. It removes suspended particles before filtration, concentration, or filling. In practice, operators often use filter vessels, centrifuges, and activated-carbon systems together. A clear syrup should not hide a weak process.
The global food processing equipment market reached about USD 58.9 billion in 2022, according to Grand View Research. Its report forecasts a 5.1% compound annual growth rate from 2023 to 2030. This expansion supports demand for hygienic clarification systems with automated controls. Pharmaceutical producers also require documented cleaning, validated filtration, and traceable contact materials under GMP guidance. Small design details matter. Dead legs, rough welds, or poor drainability can create serious cleaning risks.
Maintenance should include daily pressure checks, weekly inspection of seals, and scheduled membrane or filter replacement. Operators should record turbidity, flow rate, temperature, and differential pressure for every batch. According to the International Society for Pharmaceutical Engineering, digital monitoring and risk-based maintenance are becoming stronger industry practices. Energy efficiency is another trend, especially where syrup heating increases operating costs. Some manufacturers now combine sensors, variable-speed pumps, and remote alarms. However, automation is not perfect. A sensor can drift, and staff may trust it too quickly. Manual verification still deserves a place in the operating routine.
Syrup Clarification Equipment: Typical Operating Temperature Ranges
Syrup clarification systems commonly operate at elevated temperatures to reduce viscosity and improve filtration performance. The ranges below represent typical engineering operating windows used for process screening, precoat filtration, carbon treatment, and membrane polishing. Actual settings depend on syrup concentration, product quality targets, equipment design, and heat sensitivity.


Share On: