Blog
Signature Lawn and Landscape LLC
How to Choose the Best CNC Cutting Machine?
Choosing the right Cnc Cutting Machine can shape your workshop’s accuracy, speed, and long-term costs. The best choice depends on your materials, production volume, workspace, and operators’ skills. A compact machine may suit a sign maker, while a heavy-duty model may serve a metal fabrication shop better. Similar-looking machines can perform very differently.
Real workshop decisions require more than reading impressive specifications. Examine cutting thickness, spindle power, working area, positioning accuracy, and control compatibility. Ask how the machine performs after eight hours of continuous work. Check sample cuts on your actual materials, including plywood, acrylic, aluminum, or composite panels. Small details matter. A rough edge can create hours of extra finishing work.
Reliable manufacturers provide clear technical data, safety guidance, training, and accessible replacement parts. Independent reviews and verified customer feedback can reveal service delays that brochures rarely mention. Industry experience also shows that the cheapest machine is not always economical. However, premium pricing does not guarantee perfect results. No machine is perfect. Operators still need maintenance routines, correct tooling, and realistic production settings. Even experienced buyers can overlook noise, dust collection, software learning curves, or limited after-sales support. This guide compares these practical factors, helping you evaluate each Cnc Cutting Machine with greater confidence and fewer costly surprises. The final decision should balance measurable performance with dependable support, workplace safety, and your actual business goals.
Understanding CNC Cutting Machine Types and Their Applications
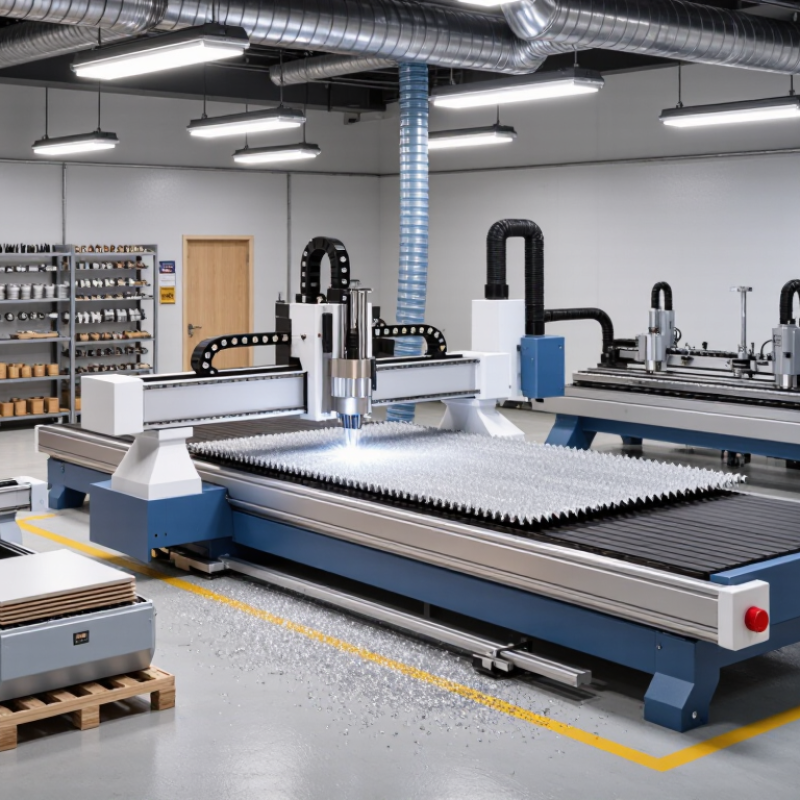
Choosing the best CNC cutting machine starts with the material, not the machine name. A CNC router suits wood, plastics, foam, and some soft composites. It uses rotating bits to create signs, panels, grooves, and three-dimensional surfaces. A laser cutter produces narrow, precise cuts in sheet materials. It works well for acrylic, plywood, fabric, and thin metals, depending on power and ventilation. Plasma machines cut conductive metal quickly, especially steel and aluminum. Waterjet systems handle thick metal, stone, glass, and heat-sensitive materials without a heat-affected edge. Each type solves a different production problem.
Tips: Test a sample before ordering. Check thickness limits, kerf width, bed size, extraction, software compatibility, and operator training. Ask for measured tolerances, not vague promises. Review maintenance access and consumable costs. A fast machine can become expensive when downtime is frequent. Keep safety guards, ventilation, and emergency controls central to the decision. They are not optional features.
Application changes the answer. A furniture workshop may value a large router bed and dust collection. A metal fabricator may need plasma speed or waterjet accuracy. A prototype shop might prefer laser detail and quick setup. In real workshops, the “best” choice is rarely perfect. Teams sometimes choose excessive power, then struggle with heat, waste, and complicated settings. Sometimes a smaller machine delivers better control. Compare actual jobs, expected volume, tolerances, and available floor space. Leave room for mistakes. Your workflow should guide the specification, not advertising language.
| CNC Machine Type | Primary Cutting Method | Suitable Materials | Typical Material Thickness | Typical Accuracy | Best Applications | Main Advantages and Limitations |
|---|---|---|---|---|---|---|
| CNC Router | Rotating cutting tool removes material mechanically. | Wood, MDF, plywood, plastics, acrylic, foam, composites, and some soft non-ferrous metals. | Usually up to 50 mm for sheet materials; heavier machines can process thicker stock. | Approximately ±0.05 to ±0.20 mm, depending on machine construction, tooling, and workpiece. | Furniture components, signs, cabinet panels, prototypes, decorative panels, and 3D carving. | Versatile and relatively economical. It produces chips and tool wear, and it is generally unsuitable for hardened steel or highly reflective metals. |
| CNC Fiber Laser | Focused laser beam melts or vaporizes material with assist gas. | Carbon steel, stainless steel, aluminum, brass, copper, and other conductive metals. | Commonly used from thin sheet to about 25 mm in carbon steel; practical capacity varies with laser power and material. | Approximately ±0.03 to ±0.10 mm under suitable operating conditions. | Sheet-metal fabrication, electrical enclosures, automotive parts, brackets, precision blanks, and intricate profiles. | Fast, narrow kerf, low mechanical force, and excellent detail on sheet metal. Initial cost can be high, and reflective materials require suitable machine configuration and process control. |
| CNC CO2 Laser | Infrared laser beam cuts or engraves non-metallic materials. | Acrylic, wood, paper, cardboard, textiles, leather, rubber, and selected plastics. | Often up to 20–30 mm for wood or acrylic, depending on power, material, and cutting speed. | Approximately ±0.05 to ±0.20 mm for many sheet and engraving applications. | Sign making, packaging prototypes, engraving, crafts, architectural models, and interior decoration. | Provides clean edges and fine engraving on many non-metals. It is not normally suitable for bare metal cutting, and some plastics can release hazardous fumes when heated. |
| CNC Plasma Cutter | High-temperature ionized gas melts conductive metal, while a gas jet removes molten material. | Carbon steel, stainless steel, aluminum, and other electrically conductive metals. | Commonly 1–40 mm; industrial systems can cut substantially thicker plate. | Approximately ±0.15 to ±0.50 mm, depending on plate thickness, torch height, consumables, and process settings. | Structural steel parts, machinery frames, agricultural equipment, repair work, and medium-to-thick plate fabrication. | Fast and cost-effective for conductive metal plate. It creates a heat-affected zone and generally has a wider kerf and lower fine-detail capability than laser cutting. |
| CNC Waterjet | High-pressure water, often mixed with abrasive garnet, erodes the material. | Steel, stainless steel, aluminum, stone, glass, ceramics, rubber, composites, and layered materials. | Commonly 1–150 mm; specialized equipment can process thicker materials. | Approximately ±0.05 to ±0.15 mm for many precision systems. | Heat-sensitive materials, thick metal, stone countertops, aerospace components, glass, and mixed-material assemblies. | No heat-affected zone and broad material compatibility. It has higher operating costs, uses water and abrasive, and is usually slower than laser for thin sheet metal. |
| CNC Oxy-Fuel Cutter | Fuel gas preheats steel, and a high-purity oxygen jet oxidizes and removes the material. | Primarily carbon steel and low-alloy steel; not suitable for aluminum or stainless steel in normal operation. | Typically about на? 6–300 mm; heavy-duty systems can process thicker plate. | Approximately ±0.50 to ±1.50 mm, depending on equipment, plate thickness, and setup. | Heavy steel plate, structural components, shipbuilding, bridges, large machinery, and demolition or repair work. | Low equipment and operating cost for very thick carbon steel. It is relatively slow, produces a large heat-affected zone, and requires careful gas handling and ventilation. |
| CNC Knife Cutter | Oscillating, tangential, or rotary knife mechanically cuts flexible or semi-rigid sheet materials. | Foam, cardboard, corrugated board, textiles, leather, vinyl, rubber, gaskets, and composite fabrics. | Commonly up to 50 mm, depending on material density and knife configuration. | Approximately ±0.10 to ±0.50 mm for many sheet-cutting applications. | Packaging, upholstery, apparel patterns, insulation, gaskets, signage, and soft-material prototyping. | Produces no thermal discoloration or melted edges and is well suited to flexible materials. It cannot cut most metals and may require specialized blades for dense materials. |
Share On: